Curated Export Portfolio & Engineering Masterpieces
Explore our trending, laboratory-certified educational toys, precision mortise-and-tenon structural assemblies, and multi-sensory magnetic sets engineered for global commercial distribution.
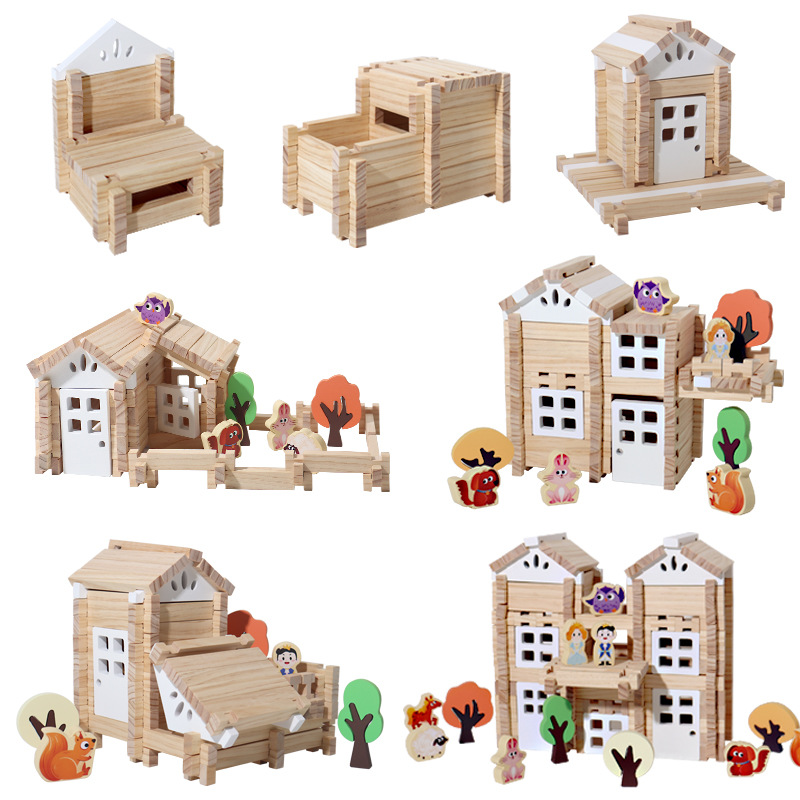
Little Architect Luban Mortise Tenon Structure Building Blocks Educational Assembled Original Wooden House for 4-6Y
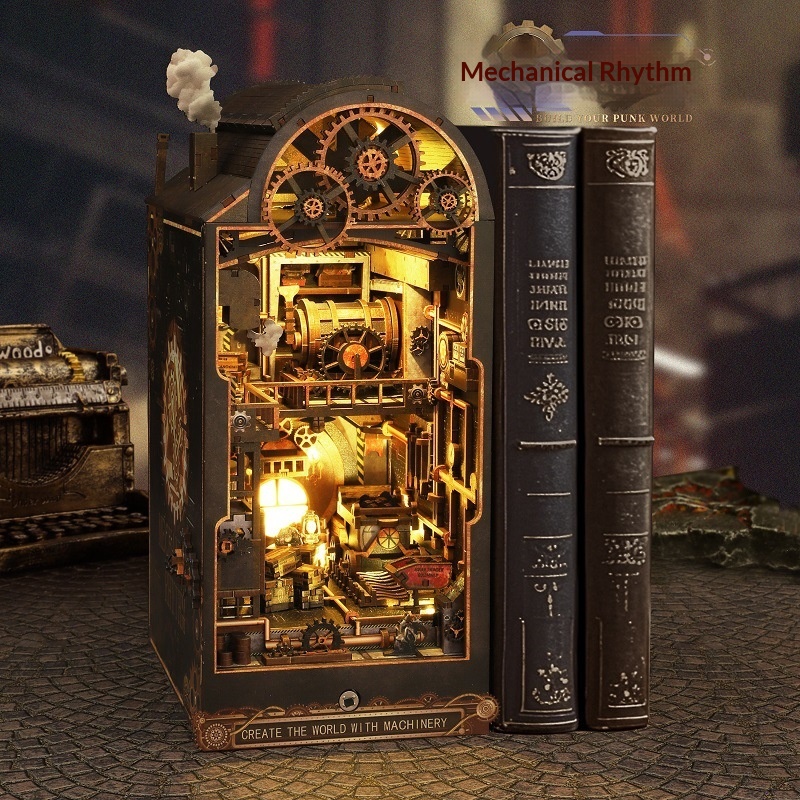
DIY Cottage Mechanical Rhythm 3D Assembled Wood Book Stand House Miniature Model Building Toy Color Box
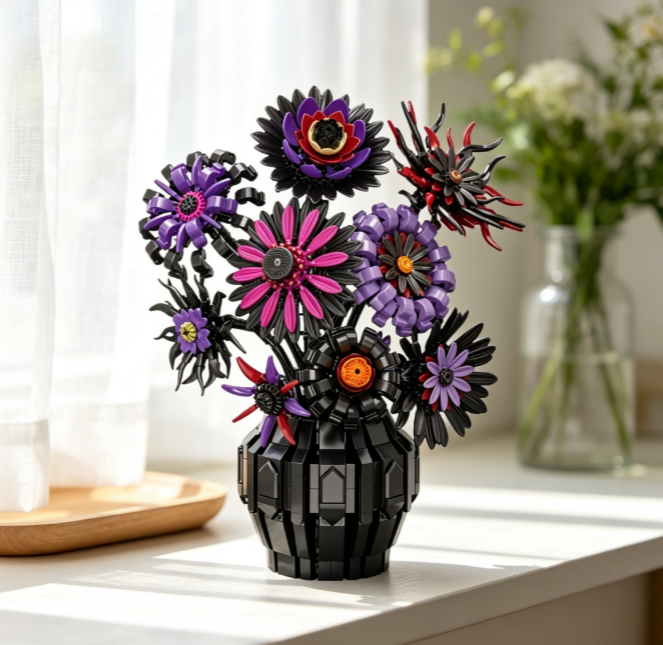
40 Piece Sunflower Building Blocks ABS Plastic Construction Toy Educational Model Home Decor Flower Bouquet 1 24 Scale
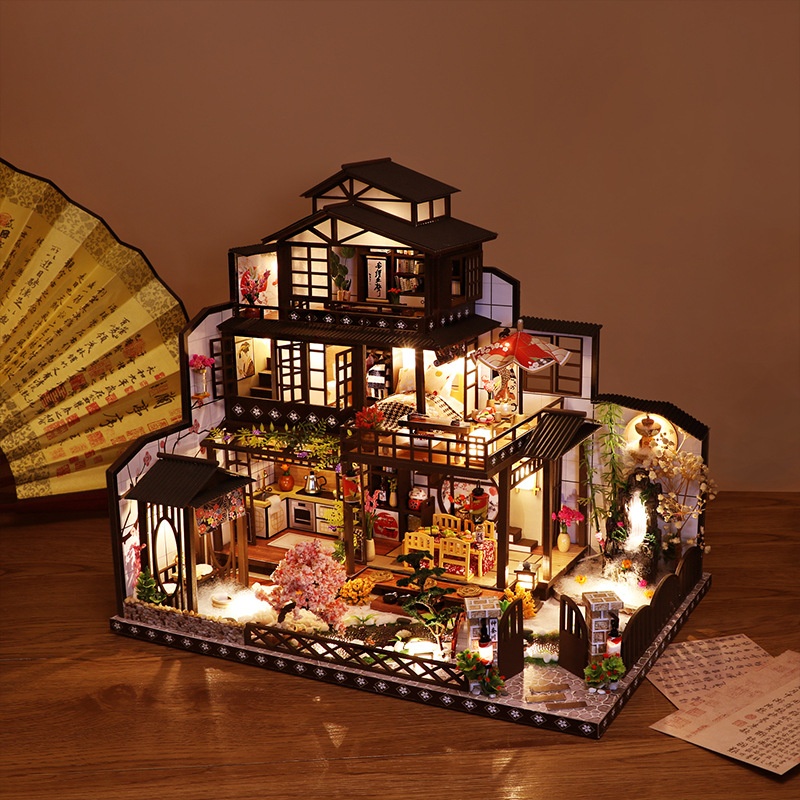
New DIY Wooden House Ancient Capital Moon Viewing Creative Retro Japanese Style Hand Assembled Building Model Villa Toy
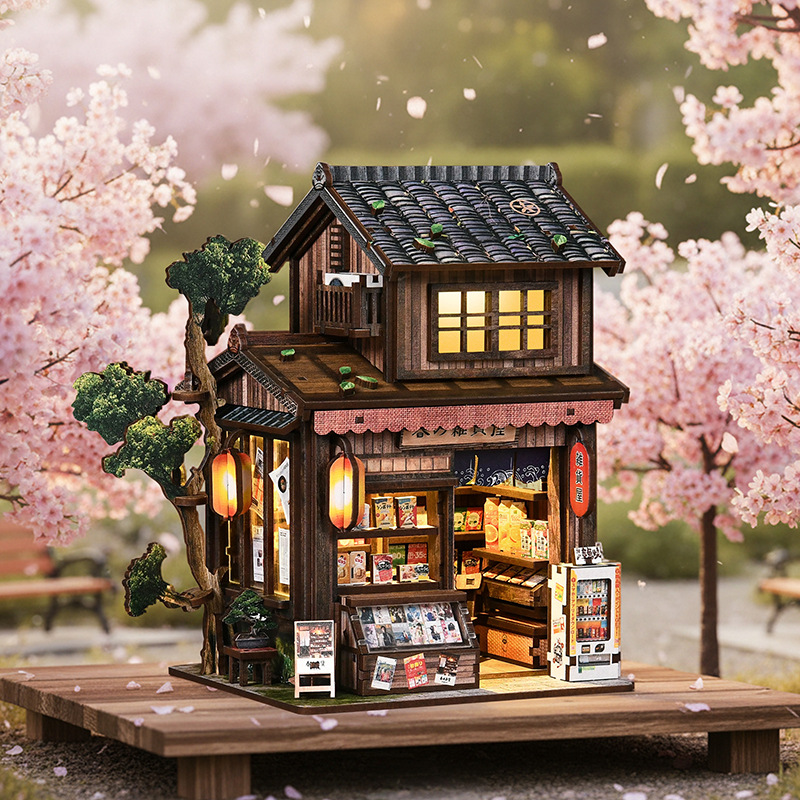
Hut DIY Spring Day Grocery Store 3D Handmade Wood Assembly Building Model Creative Toy Gift House Decoration
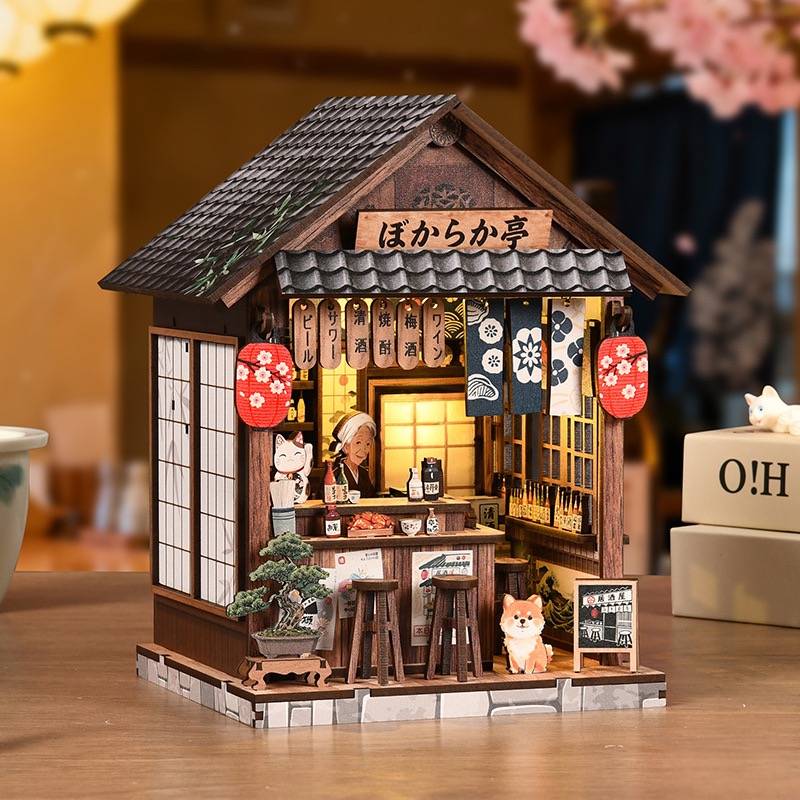
DIY Yiran Izakaya 3D Handmade Assembly Wood Building Model Creative Toy Gift House Decoration Color Box
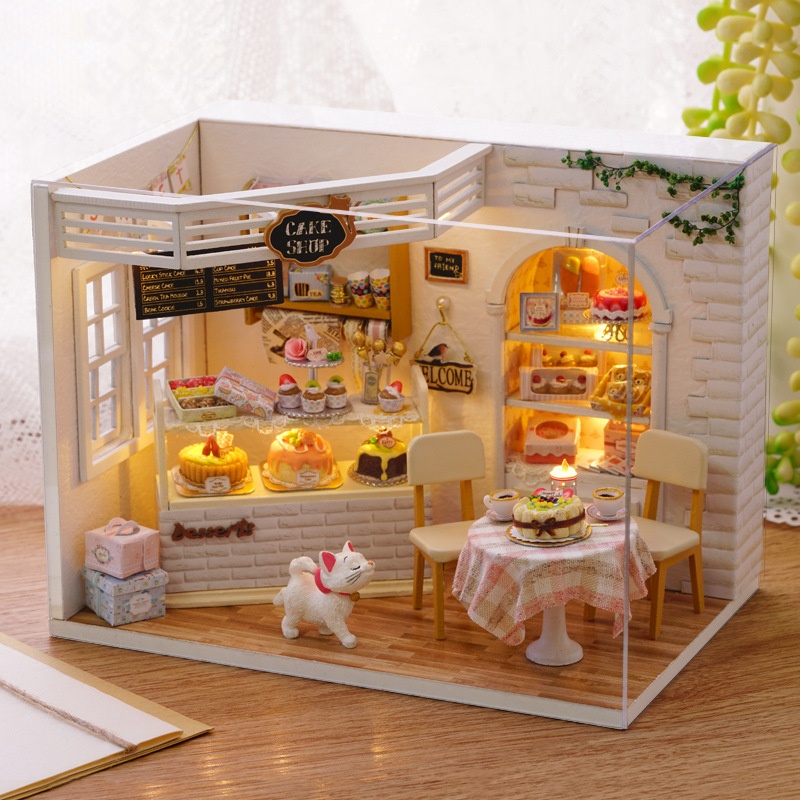
Smart Fun House DIY Cake Diary Cottage Wooden Finished Model Gift for Boys and Girls Birthday Creative Building
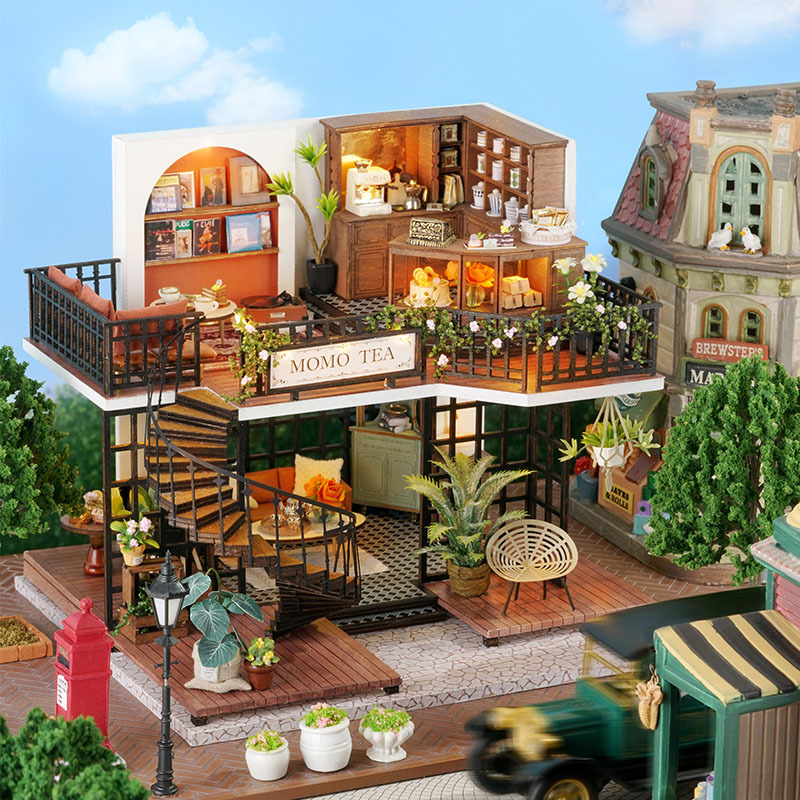
Smart Fun House DIY Jungle Momo Tea Retro Main Double-Story Villa Wood House Model Gift
Executive Summary: The Industrial Evolution of EVA Magnetic Building Blocks
The global educational toy landscape has experienced a paradigm shift, transitioning from rigid ABS construction kits toward flexible, tactile, and sensory-driven construction media. Among these innovations, EVA (Ethylene-Vinyl Acetate) magnetic blocks have emerged as an indispensable cornerstone in early childhood education (ECE), institutional preschool curricula, and home developmental playrooms. Unlike conventional brittle plastics or unyielding timber, high-density closed-cell EVA copolymer provides exceptional impact attenuation, high buoyancy for hydro-sensory interaction, sound deadening during energetic play, and intrinsic thermal retention.
From an engineering and B2B procurement perspective, the technical complexity of modern magnetic EVA blocks lies far beyond simple foam die-cutting. Professional tier-1 Chinese manufacturers utilize proprietary encapsulation metallurgy and ultrasonic rotational fusion to completely seal permanent NdFeB (Neodymium-Iron-Boron) magnets inside impermeable internal chambers. This engineering feat eliminates magnetic detachment hazards while maintaining a flux index compliant with worldwide product liability frameworks—including ASTM F963-17 Clause 4.38 and European Standard EN 71-1:2014+A1:2018. As global educational buyers require verifiable safety dossiers, selecting an experienced manufacturer with proven export infrastructure is the baseline requirement for mitigating regulatory risks in Tier-1 consumer markets.
Material Engineering, Magnet Safety Standards & Quality Control Matrix
To qualify for tier-one distribution in North America and Western Europe, the chemical composition and physical durability of EVA magnetic assemblies must survive severe environmental torture testing. Standard open-cell foamed rubber is susceptible to microbial colonization, saliva plasticization, and rapid polymer degradation under UV light. Premium manufacturers exclusively specify high-purity, closed-cell, crosslinked EVA copolymer featuring a vinyl acetate content calibrated between 18% and 28%. This specific macromolecular balance delivers an optimal Shore durometer hardness (ranging from 35C to 50C), yielding a resilient tactile touch that resists puncture by emerging deciduous teeth while maintaining structural stability under heavy mechanical loading.
The cornerstone of pediatric safety in magnetic building toys resides in flux density limitation and mechanical detachment prevention. Under international directives, any ingested magnetic component presenting a magnetic flux index exceeding 50 kG²mm² (0.5 T²mm²) presents a severe intestinal perforation hazard should two or more pieces be swallowed. Aitoybots and top Chinese manufacturing hubs employ a three-tier defense mechanism:
| Evaluation Parameter | Export Compliance Target | Testing Protocol / Benchmark | Engineering Solution Implemented |
|---|---|---|---|
| Magnet Encapsulation Tensile Force | > 90 N (Zero Dislodgement) | EN 71-1 Tension Test & ASTM F963 Torque | Dual-layer injection molded POM core welded hermetically within EVA body |
| Magnetic Flux Index | < 50 kG²mm² (Safe Limit) | Digital Gaussmeter / Hall Probe Surface Field | Calibrated N35/N38 sintered NdFeB with isotropic flux orientation |
| Volatile Organic Compounds (VOC) | Formamide < 200 mg/kg | French Arrêté & EU Toy Directive 2009/48/EC | Secondary continuous hot-air degassing post-foaming cycle |
| Shore Hardness & Compression Set | 38C – 45C (< 15% 22h @ 23°C) | ASTM D395 Method B Compression Deflection | Virgin crosslinked PE/EVA hybrid matrix formulation |
| Heavy Metals & Phthalate Ester | ND (Below Instrument Limits) | CPSC-CH-C1001-09.4 & EN 71-3 ICP-MS | Eco-friendly organic color masterbatch with REACH SVHC sign-off |
Beyond material purity, our quality control protocols include continuous tumble drop testing from 1.5 meters onto hardened steel plates, submerged hydrostatic pressure checks to verify airtightness, and prolonged salt-spray immersion to prevent magnet oxidation within tropical distribution hubs.
Future Procurement Trends: Where the EVA Magnetic Market is Heading
Category managers, educational toy brand owners, and multinational procurement directors must anticipate shifting consumer expectations, strict ecodesign mandates, and evolving educational curricula over the 2025–2030 planning horizon.
1. Bio-Circularity & Carbon Neutrality
Global demand is accelerating toward bio-based EVA derived from sugarcane molasses or post-consumer recycled polyolefins, shrinking lifecycle carbon footprints without sacrificing soft-play shock absorption.
2. Hybrid Material Synergy
The convergence of warm natural beech/basswood timbers with compliant magnetic EVA edges creates heirloom structural integrity coupled with silent, soft-contact assembly dynamics.
3. STEAM Spatial Geometry Integration
Moving past basic geometric cubes, contemporary sets incorporate polyhedral architecture, geodesic vertices, and magnetic interlocking trusses that demonstrate real-world civil engineering fundamentals.
4. Inclusive & SEN Adaptive Play
Sensory-friendly classrooms require silent, soft-landing toys for neurodiverse children. EVA magnetic arrays satisfy tactile stimulation needs without triggering auditory sensory overstimulation.
Enterprise Strengths & Export Infrastructure
Combining heritage craftsmanship with modern engineering since 2011 to empower global toy brands, retail chains, and educational institutions.
Heirloom Craftsmanship Since 2011
Originating from a dedicated Jinhua woodworking workshop in 2011, Hangzhou Aitoybots Trading Co., Ltd. has spent over 14 years mastering ancient structural mechanics—such as classical Luban mortise and tenon joinery—and integrating them with cutting-edge STEM pedagogical principles.
80% Global Export Specialization
Our operational pipeline is meticulously geared toward European and North American customs clearance standards. Over 80% of our annual production volume ships directly to German, French, British, American, and Canadian brand owners, wholesale distributors, and museum gift channels.
Rigorous 0.3% Defect Threshold
By implementing an exhaustive 6-stage Quality Control protocol—encompassing incoming raw EVA/wood spectroscopic assay, automatic magnetic pole alignment verification, ultrasonic weld shear testing, drop testing, and hand packaging inspection—we maintain an industry-leading defect rate below 0.3%.
Agile ~30-Day Turnaround & Flexible MOQ
We respect dynamic supply chains. Catalog baseline orders start from small trial lots of 2 to 20 pieces per SKU to validate marketplace sell-through, while full container OEM custom tooling and production projects reliably deliver within an average window of 30 days post-sample approval.
Full OEM/ODM Engineering & Custom Packaging
Our in-house industrial engineering department assists B2B clients from 3D CAD modeling, custom durometer adjustment, Pantone color matching, private-label silk-screen/heat-transfer graphics, to eco-friendly FSC-certified retail window carton engineering.
Educational Institution Accreditation
Trusted by more than 50 educational supply foundations and 200+ specialized e-commerce brands, our toys are engineered to be passed down across generations—delivering tactile screen-free problem solving that nurtures creative resilience.
Frequently Asked Questions for B2B Importers
Essential regulatory, technical, minimum order, and supply-chain logistics answers to streamline your international sourcing audit.
Every production batch is certified against CE marking requirements, European Toy Safety Directive (EN 71 Parts 1, 2, and 3 - migration of 19 heavy elements), REACH Annex XVII, and French VOC decrees. For North American importation, full documentation for ASTM F963-17/F963-23, CPSIA (Total Lead Content & 8P Phthalates), and California Proposition 65 is provided through accredited testing laboratories (SGS, TÜV Rheinland, or Intertek).
We reject topical adhesive bonding. Our factory utilizes a dual-barrier mechanical lock: the sintered neodymium magnet is encapsulated within an injection-molded, shatterproof Polyoxymethylene (POM) inner capsule. This core is then positioned inside the closed-cell EVA preform and hermetically sealed via high-frequency ultrasonic induction welding, creating a monolithic seal that withstands sustained tensile forces exceeding 120 N.
To empower specialty boutique toy stores and digital marketplace test launches, standard catalog inventory items start at a low MOQ of just 2 to 20 pieces per SKU. For bespoke OEM/ODM programs requiring custom EVA die-cut tooling, tailored color pigments, and branded color-box packaging, custom MOQs typically start at 500 to 1,000 sets per project.
Pre-production rapid prototyping samples require 5 to 7 working days. Once the golden sample and structural packaging proofs are authorized, bulk assembly timelines average approximately 30 calendar days. We routinely support consolidated container loading (FCL/LCL), DDP air-cargo drop delivery, and bonded warehousing handoffs directly from Ningbo and Shanghai maritime ports.
Yes. Due to the hydrophobic properties of our closed-cell crosslinked ethylene-vinyl acetate formulation, moisture cannot infiltrate the internal structural cells. The blocks can be submerged during water-table sensory play, rinsed with standard mild soap, and disinfected using sanitizing solutions without suffering rot, swelling, adhesive breakdown, or internal magnet oxidation.
Yes. Aitoybots started as a precision woodworking atelier in 2011. We possess proprietary CNC machining and laser-cutting capacity to craft hybrid sets combining FSC-certified solid beechwood, basswood structural components, and high-density magnetic EVA connectors, giving your brand an exclusive design edge in competitive retail markets.
Partner with China's Premier Educational Toy Manufacturer
Accelerate your product launch with low entry MOQs, verified laboratory compliance certificates, and factory-direct pricing backed by 14+ years of engineering craftsmanship. Our multilingual account executives are standing by to review your Bill of Materials (BOM) and deliver rapid quotations.
Get a Quote